Laxmi Conveyor is a trusted name in the material handling industry, known for designing smart and efficient solutions for modern warehouses and distribution centers. We design systems that offer smooth, reliable, and efficient movement of materials across various operational stages. One of the most effective solutions today is the monorail conveyor, a system that brings both efficiency and flexibility to handling goods. We continue to offer advanced solutions that help businesses streamline their operations with ease.
What Is a Monorail Overhead Conveyor?
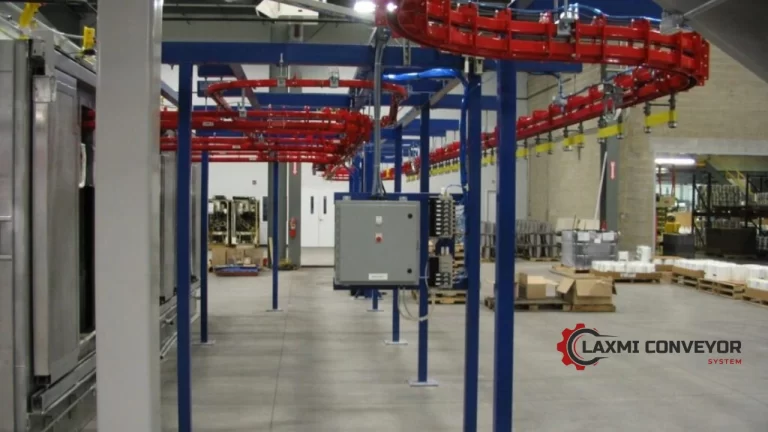
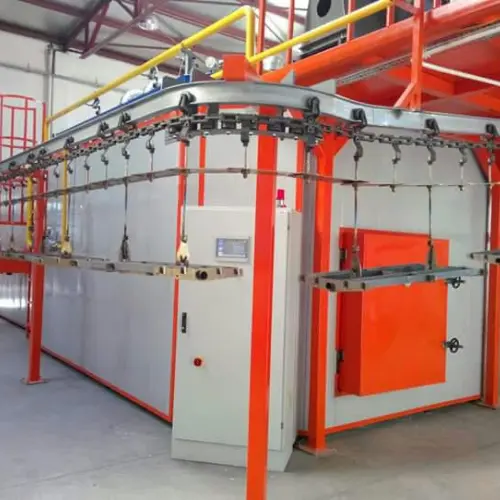
A monorail overhead conveyor is a material handling system installed above the working area. It generally uses a continuous track along which carriers, trolleys, or other load-supporting components travel. Instead of moving products along the floor, the system carries them overhead from one point to another. Depending on the design, products can be transported between different departments, workstations, storage areas, and dispatch zones.
This arrangement can be especially useful in facilities where floor space is already occupied by machinery, racks, pallets, workers, or vehicles.
Why Choose Monorail Conveyors for Warehouses?
There are several reasons why businesses consider monorail conveyors for warehouse and distribution operations. The biggest advantage is that they make use of space that is otherwise largely unused—the area above the floor.
1. Saves Valuable Floor Space
Warehouse floor space is expensive and needs to be used carefully. Traditional transportation methods can require clear pathways for forklifts, carts, and manual handling.
An overhead system moves materials above these pathways, allowing valuable floor space to remain available for storage, production, walking routes, and other activities.
2. Creates a Continuous Material Flow
A warehouse becomes more efficient when products can move between different stages without unnecessary interruptions. An overhead monorail can create a defined route for materials, reducing the need for workers to repeatedly transport products manually.
This can help maintain a more consistent flow from one operation to another.
3. Reduces Manual Material Movement
Carrying or pushing materials across a large distribution center can consume considerable time. It can also make repetitive jobs tiring for employees. An overhead conveyor can handle much of this repetitive transportation work. Workers can then concentrate on activities such as inspection, picking, packing, loading, and inventory management.
4. Helps Reduce Floor-Level Congestion
Forklifts, carts, pallets, and employees often share the same floor area in busy warehouses. During peak operating periods, this can create congestion and make material movement slower.
Since the conveyor operates overhead, materials can follow a separate transportation route. This can help keep floor-level traffic more organized.
5. Suitable for Repetitive Routes
If the same products need to travel between the same locations throughout the day, an overhead monorail can be a practical choice.
Applications of Overhead Monorail Systems
Monorail systems are not limited to a single type of warehouse. Their configuration can be adapted for different material handling requirements.
They can be used for:
- Distribution centers
- Warehouses
- Manufacturing plants
- Automotive facilities
- Garment industries
- Assembly operations
- Packaging facilities
- Storage and dispatch areas
- Component handling
- Process-to-process transportation
The system can also be designed with curves, inclines, switches, or different track arrangements depending on the layout of the facility.
Why Choose Laxmi Conveyor?
Every warehouse has its own layout and material movement challenges, so a standard approach may not always provide the best result. Laxmi Conveyor focuses on practical conveyor and material handling solutions designed around the needs of individual facilities. Our company can offer suitable overhead conveyor solutions for businesses looking to improve material flow, reduce unnecessary floor-level movement, and make better use of available warehouse space. By understanding the product type, transportation route, load requirements, and facility layout, businesses can select a configuration that supports their operational goals.
An overhead monorail conveyor can be a smart option for distribution centers and warehouses that need organized, continuous material movement without sacrificing valuable floor space. It can help reduce manual transportation, minimize floor congestion, improve workflow, and create a more predictable movement path for products. For businesses looking to improve their internal material handling process, a well-designed monorail overhead conveyor can be more than just a transportation system—it can become an important part of a faster, cleaner, and better-organized warehouse operation.